MetalsAlloy
How Can You Anneal or De-Nitride Plasma Cut A36 Steel Edges at Home?
Published:
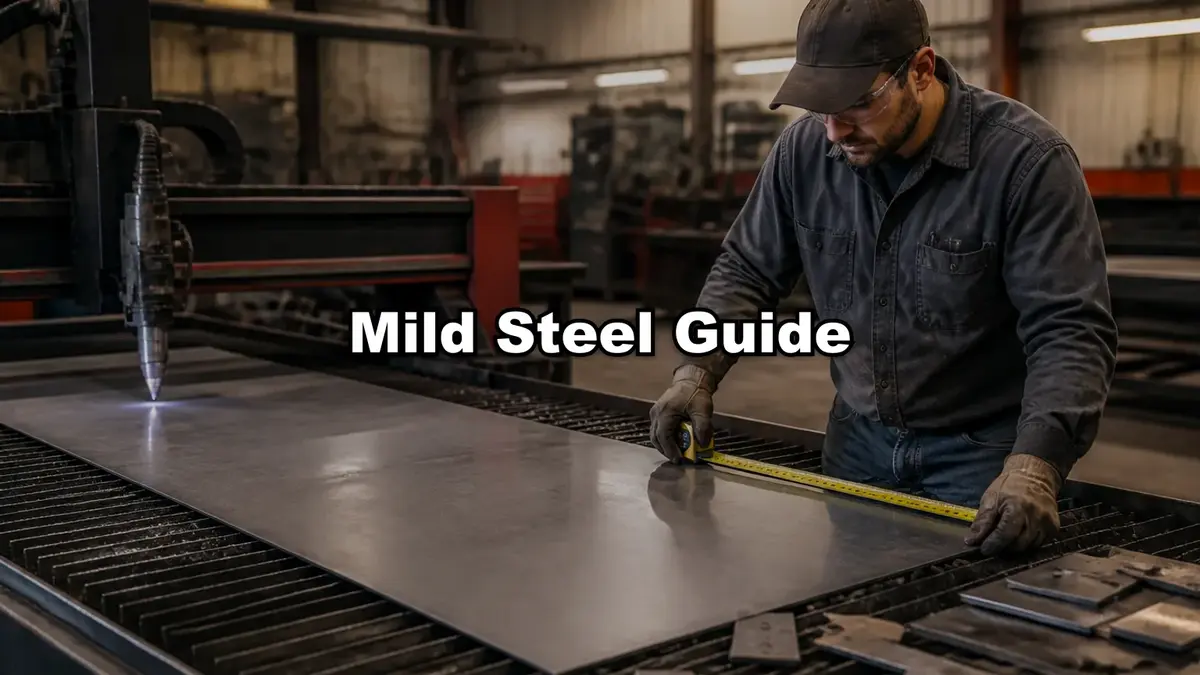
Direct Answer: Can You Anneal or De-Nitride Plasma Cut A36 Steel Edges at Low Tech Shops?
After plasma cutting, the edges of A36 steel plate become hard and sometimes brittle due to rapid heating and cooling, and in some cases, surface nitriding. If you want to soften these edges for machining or welding—conventional kitchen oven temperatures are not sufficient for full annealing or de-nitriding of A36 steel. Low-cost, low-tech approaches can help, but each comes with trade-offs. See below for details and practical recommendations.
What Happens to A36 Steel During Plasma Cutting?
Alloy, Temper, and Use Case
- Alloy: ASTM A36 is a common low-carbon structural steel, usually supplied in hot-rolled plate, flat bar, and structural shapes.
- Temper/Condition: Supplied as rolled (not heat-treated). After plasma cutting, only the cut edge (the heat affected zone or HAZ) is hardened and potentially nitrided.
- Problem: Plasma cutting exposes the cut edge to extremely high temperatures (up to 40,000°F at the arc), followed by rapid cooling. This produces:
- A hardened HAZ: Increased difficulty for further machining/drilling.
- Surface nitriding: Nitrogen from air plasma can react at high temperature, creating a thin, brittle, hard surface layer.
- Potential for microcracks: Especially if you need to weld near the cut edge.
What Does This Mean for Workshop Tasks?
Most A36 steel remains its usual soft, machinable self—except right at the plasma cut edge, where you may encounter brittle or extra-hard material that quickly ruins tools or resists weld penetration.
Full Annealing: What Actually Works?
What Is Required for True Annealing?
Annealing A36 steel requires:
- Heating above the transformation (critical) temperature—typically 1550–1600°F (840–870°C).
- Holding at temperature (soaked) long enough for even heating.
- Very slow cooling, usually by leaving the steel in a switched-off oven/furnace to come down to ambient temperature.
At these conditions, the internal structure of steel changes (from pearlite/ferrite to austenite, then reforms as softer pearlite/ferrite), eliminating HAZ hardening and increasing ductility.
Can a Kitchen Oven Anneal or De-Nitride Plasma Cut A36?
No.
- Kitchen ovens max out around 500°F (260°C). A36 steel requires more than three times this temperature to anneal.
- Multiple cycles at kitchen oven temperatures might slightly temper stressed regions but will NOT remove the hard, brittle HAZ or nitride layer.
Is There a Low-Tech Option Without Industrial Furnaces?
Industrial heat-treating ovens or forges are ideal, but some home and shop options include:
1. Propane/Fuel Torch Annealing or Campfire/Barbecue Method
- Use a propane or oxy-fuel torch, BBQ, or bonfire to heat the entire part or just the affected edges until it reaches a dull red (about 1400–1600°F or 760–870°C).
- Maintain temperature evenly across the HAZ. Avoid concentrating the heat in a small spot, as this can cause warping.
- Once at temperature, cover the part—burying in ashes, vermiculite, or insulating blanket (e.g., Kaowool or ceramic fiber)—to slow down the cooling as much as possible.
- Allow to cool to room temperature over several hours. Fast cooling (air or water quenching) will not soften the steel.
Drawbacks:
- Parts may warp during heating/cooling, especially thin or uneven geometries.
- Difficult to control temperature precisely without a furnace or thermocouples.
- Large, thick sections are challenging to heat evenly.
2. Localized Heating with Torch
- For localized softening, a torch can be used to heat just the edge.
- This is less effective than full annealing, may not fully eliminate the HAZ hardness or nitride layer, and can risk distortion near the cut.
3. Removing the Hard/Brittle Edge by Machining or Grinding
- A practical alternative to annealing is to machine or grind away the HAZ.
- Use a grinder, aggressive carbide cutters, or cobalt roughing end mills to remove 1–2 mm from the cut edge.
- After rough removal, a standard cutter can finish the operation.
Advantages:
- No risk of warping.
- Quick and effective when geometry allows.
- For thick plates, conventional milling with strong feed and conventional (not climb) milling is preferred.
Disadvantages:
- You must have enough material at the edge.
- Tool wear can be high if not aggressive enough.
4. Can Lower Temperature Ovens (e.g., 350–425°F) Help?
- Very limited effect.
- Tempering at 350–425°F may slightly reduce brittleness if significant stresses are present, but will not remove the hard HAZ or nitrided layer.
- Repeated low-temp oven cycles have negligible real benefit on plasma cut A36 compared to full annealing or mechanical removal.
Table: Methods for Removing Plasma Cut Edge Hardness on A36 Steel
| Method | Temperature Range | Effectiveness | Notes |
|---|---|---|---|
| Kitchen oven cycles | ~350–500°F (175–260°C) | Not effective | Does not anneal or denitride edges |
| Propane torch/campfire | ~1400–1600°F (760–870°C) | Effective if slow cooled | Risk of part warping; hard for large pieces |
| Industrial furnace annealing | 1550–1600°F (840–870°C) | Very effective | Best, but seldom available in small shops |
| Mechanical removal (grind/mill) | N/A | Highly effective | Fast, but needs excess material at edges |
Plasma Cut Edge Hardening vs. Oxy-Fuel Cut Edges
- Plasma cutting results in harder, more brittle HAZ vs. oxy-fuel cutting, even on mild steel.
- The rapid heat/cool cycle is a primary cause, but atmospheric nitrogen at the plasma arc creates a thin nitride layer that is both harder and more challenging for subsequent welds or machining tasks.
- Oxy-fuel (flame) cutting uses lower temperatures, causes less nitriding, and is generally easier to machine at the cut edge afterward.
Is De-Nitriding Possible With Simple Heating?
- The thin nitride layer created by plasma cutting is especially stubborn. Annealing (at correct high temperature) will temper or remove much of the HAZ hardness, but may not completely remove nitride compounds.
- Grinding or heavy milling remains the most reliable way to eliminate both hard and nitrided regions if you cannot access industrial heat treatments.
Minimizing the Problem in Production
Best Practice:
- Cut parts with excess material at the perimeter to allow removal of plasma cut edges.
- Choose oxygen plasma or shielded gas cutting processes if possible; they reduce nitriding.
- Consider changing to oxy-acetylene or mechanical processes for finish-sensitive edges.
Frequently Asked Questions
Q: Can you use a self-cleaning oven’s high temperature cycle to anneal A36 steel?
A: No. Even self-cleaning ovens only reach around 900°F (480°C), which is well below A36’s annealing range.
Q: Is stress-relieving (tempering) enough?
A: Tempering at low temperatures may reduce internal stresses but will not effectively soften the plasma cut HAZ or remove the hard nitride layer.
Q: Does burying hot steel in ashes really help slow-cool it?
A: Yes, insulation (ashes, vermiculite, ceramic blanket) slows cooling and helps achieve a softer, annealed result during home-annealing attempts, but precise control is hard without a real furnace.
Summary: Practical Pathways for Workshop Users
If you must soften plasma cut A36 steel edges without professional equipment:
- Kitchen oven and similar low-temperature approaches are NOT effective for annealing or de-nitriding.
- For home/small shop work, use aggressive grinding or carbide/conventional roughing mills to remove the brittle edge.
- If full softening is essential, attempt torch or barbecue annealing followed by slow insulation-cooled cooling, understanding the risk of warping and incomplete softening.
- Industrial facilities with real heat-treating furnaces remain the gold standard for full annealing.
Proper method selection depends on your part geometry, available equipment, and tolerance for warping or tool wear. For most A36 steel forms (plate, bar, structural shapes) in as-supplied condition, mechanical removal of the HAZ is usually the quickest and most reliable approach until genuine high-temperature annealing is available.
If I clean the piece extremely well, can I expect to get rid of the nitrided sections by sticking it in the oven with dinner?
References
Annealing – Metallurgy. (n.d.). mhcc.pressbooks.pub. https://mhcc.pressbooks.pub/metallurgy/chapter/annealing
Annealing (materials science) - Wikipedia. (n.d.). en.wikipedia.org. https://en.wikipedia.org/wiki/Annealing_(materials_science)
Annealing/de-nitriding plasma cut A36 steel. (n.d.). weldingweb.com. https://www.weldingweb.com/threads/annealing-de-nitriding-plasma-cut-a36-steel.722177
Changes in mild steel hardness after cutting. (n.d.). plasmaspider.com. https://plasmaspider.com/viewtopic.php?t=21940
General | how to soften plasma cut steel | Practical Machinist - Largest Manufacturing Technology Forum. (n.d.). practicalmachinist.com. https://www.practicalmachinist.com/forum/threads/how-to-soften-plasma-cut-steel.265774
How metal fabricators can achieve plasma-cut edge perfection. (n.d.). thefabricator.com. https://www.thefabricator.com/thefabricator/article/plasmacutting/how-metal-fabricators-can-achieve-plasma-cut-edge-perfection
If I have 01 Tool Steel cut into shape with a plasma table ... (n.d.). reddit.com. https://www.reddit.com/r/knifemaking/comments/60864b/if_i_have_01_tool_steel_cut_into_shape_with_a
Plasma Cut Work Hardening. (n.d.). hobby-machinist.com. https://www.hobby-machinist.com/threads/plasma-cut-work-hardening.119273